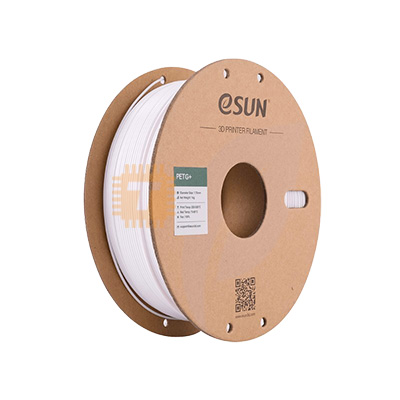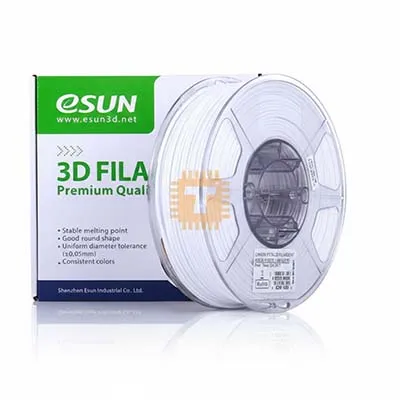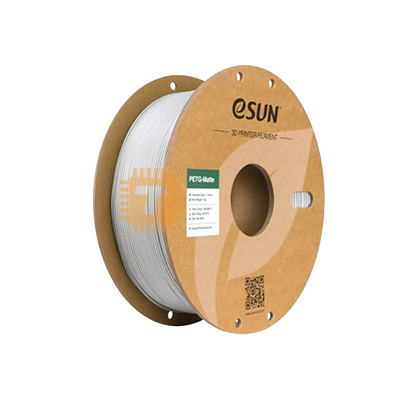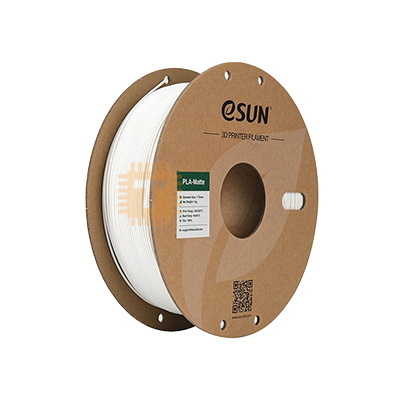
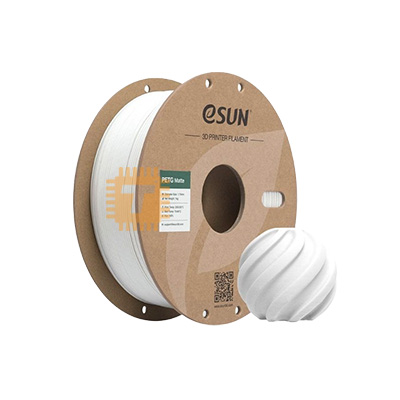
eSUN PETG-Matte White 1.75mm 1Kg 3D Printer Filament Price in Sri Lanka
Tronic.lkListing · checkedChecked 10 Nov 2026
Rs4,400Out of stock
Go to Tronic.lk ↗https://tronic.lk/product/esun-petg-matte-white-1-75mm-1kg-3d-printer-filamentCall0777854444WhatsApp+94764485607
Search for it on
Price history
Price at Tronic.lk at the end of each day · last 90 daysNo price history yetWe started tracking this listing recently. The chart and change tables appear after the first price or stock change.
Price insights
- Today at Tronic.lk
- Rs4,400
Description
The eSUN PETG-Matte White 1.75mm 1Kg 3D Printer Filament is an advanced engineering-grade thermoplastic polyester filament formulated to combine the mechanical resilience, thermal endurance, and chemical inertness of PETG with an ultra-smooth, non-glare diffuse matte surface finish. Engineered with specialized micro-matting and light-diffusing additives, it eliminates the plastic-like gloss and prominent layer-line reflections typical of standard PETG, producing clean, injection-molded-style aesthetic surfaces. Mounted on an eco-friendly recyclable cardboard spool, this 1.75mm filament features consistent extrusion tolerances (±0.03mm), high inter-layer cohesion, minimal warping, and a pure, chalk-white matte presentation suited for architectural models, consumer device housings, and functional prototypes.
Specifications
- Material Formulation: Micro-Textured Glycol-Modified Polyethylene Terephthalate (PETG-Matte)
- Filament Color : Matte White
- Filament Diameter: 1.75 mm (±0.03 mm high-precision laser-controlled tolerance)
- Net Material Weight: 1.0 kg (1000 g / ~2.2 lbs net filament mass)
- Density: Approx. 1.25 to 1.27 g/cm³
- Thermal Characteristics:
- Extrusion / Nozzle Printing Temperature: 220°C to 240°C (Recommended baseline: 230°C to 235°C)
- Heated Bed Temperature: 70°C to 80°C (Recommended baseline: 75°C)
- Heat Deflection Temperature (HDT): Approx. 65°C to 68°C (at 0.45 MPa)
- Glass Transition Temperature (Tg): ~78°C to 80°C
- Mechanical Performance:
- Tensile Strength: ≥ 40 to 45 MPa
- Elongation at Break: ≥ 80% to 110% (High ductility with enhanced rigidity compared to standard gloss PETG)
- Flexural Modulus: ~2200 MPa
- Izod Notched Impact Strength: Approx. 5.5 to 6.5 kJ/m²
- Printing Speed Compatibility: 40 mm/s to 100 mm/s (Standard kinematics) / Up to 150–200 mm/s on tuned high-speed CoreXY platforms
- Cooling Fan Speed: 30% to 60% (Moderate fan speeds preserve inter-layer tensile strength; higher speeds sharpen bridging details)
- Spool Construction: Recyclable Eco-Friendly Cardboard Spool equipped with filament level monitoring windows
- Spool Dimensions: Approx. 200 mm Outer Diameter × 65 mm Width (Arbor hub bore: ~53 mm)
- Packaging: Vacuum-sealed moisture-barrier bag with silica gel desiccant pouch in corrugated packaging
- Gross Package Weight: Approx. 1.25 kg to 1.30 kg
Features
- Superior Layer Line Camouflage: The matte light-diffusing formulation scatters specular reflections across exterior surfaces, obscuring micro-layer steps and seam lines for a smooth, mold-like visual texture.
- Non-Glossy Tactile Feel: Delivers a clean, dry-touch surface that resists fingerprint smudges, oil transfer, and glossy wear spots common on hand-held components.
- Reduced Stringing Tendency: Specialized formulation exhibits a slightly lower melt elasticity than ultra-glossy PETG, helping reduce stringing, nozzle weeping, and fine wisps across travel moves.
- Interlayer Adhesion & Durability: Maintains PETG's characteristic thermal fusion across layer boundaries, resisting shear delamination under mechanical and cyclic stress.
- Chemical, Oil & UV Resistance: Withstands dilute acids, cleaning alcohols, grease, and direct outdoor sunlight without rapid chalking or UV degradation.
- Low Warping Behavior: Low coefficient of thermal expansion facilitates flat, stable printing on both enclosed machines and open-frame printers without aggressive corner lifting.
Common Applications
- Consumer Electronics & Wearables: High-finish enclosures, IoT sensor housings, remote cases, and handheld instruments requiring an anti-glare, premium aesthetic.
- Architectural & Exhibition Models: Scale building walls, topographic dioramas, and display props requiring uniform matte white coloring without post-print sanding or priming.
- Home Automation & Wall Plates: Smart switch frames, thermostat brackets, and sensor mounts designed to blend flush with interior matte drywall surfaces.
- Industrial Jigs & Shop Fixtures: Low-reflection inspection fixtures, optical alignment brackets, and camera shroud brackets.
- Custom Medical & Laboratory Shells: Non-implantable lab device housings, fluidic manifold covers, and diagnostic equipment enclosures.
Usage Tips
- Bed Adhesion & Plate Protection (CRITICAL):
- Do NOT print directly on bare, smooth PEI or plain glass plates without a release barrier. PETG chemistry can over-adhere to smooth surfaces, potentially lifting the PEI film or tearing glass chunks during part removal.
- Use a Textured Powder-Coated PEI flex sheet or apply a thin, even coat of PVP glue stick or Magigoo as a sacrificial interface.
- Allow the bed to cool down below 35°C before attempting removal; the thermal contraction will naturally break the bond.
- Temperature Management for Matte Texture:
- Print temperature directly affects the finish: Lower temperatures (220°C–230°C) enhance the flat, diffuse matte look, while higher temperatures (≥ 245°C) increase melt sheen and reduce the matte effect.
- Run a small temperature tower to determine the ideal balance between matte texture and inter-layer bond strength for your specific hotend.
- Z-Offset Calibration:
- Avoid over-squishing the first layer. Increase Z-offset by roughly +0.02 mm to +0.03 mm compared to standard PLA bed tramming to prevent molten filament from scraping the nozzle exterior and dropping stray blobs.
- Moisture Sensitivity & Drying:
- Matte-additive PETG remains hygroscopic. Absorbed atmospheric moisture can lead to surface voids, brittle layers, and fine filament popping at the nozzle.
- Dry humid spools in an active filament dryer at 60°C to 65°C for 6 to 8 hours, and keep the roll in a sealed desiccant container during extended print jobs.
- Retraction Configuration:
- Direct-drive extruders: 0.8 mm to 1.2 mm at 35–45 mm/s.
- Bowden systems: 3.5 mm to 5.0 mm at 40–50 mm/s.
- Enable "Wipe while retracting" and keep "Avoid Crossing Perimeters" active to route nozzle travel moves inside internal infill boundaries.
Questions
About this listing at Tronic.lkWhat is the price of eSUN PETG-Matte White 1.75mm 1Kg 3D Printer Filament at Tronic.lk in Sri Lanka?
Rs 4,400, checked 10 Nov 2026.
Is eSUN PETG-Matte White 1.75mm 1Kg 3D Printer Filament in stock at Tronic.lk in Sri Lanka?
No, it was out of stock at Tronic.lk at the last check.
Where can I buy eSUN PETG-Matte White 1.75mm 1Kg 3D Printer Filament in Sri Lanka?
Tronic.lk sells it on tronic.lk. You can also call or WhatsApp the shop during opening hours.
Rs4,400at Tronic.lk · Out of stock
Go to Tronic.lk ↗https://tronic.lk/product/esun-petg-matte-white-1-75mm-1kg-3d-printer-filament