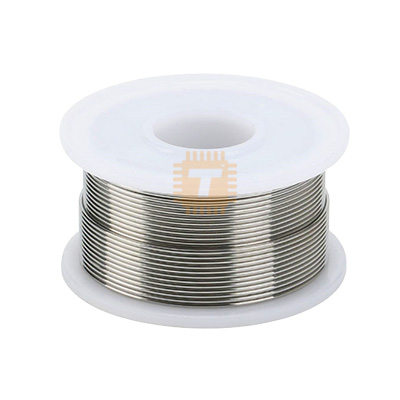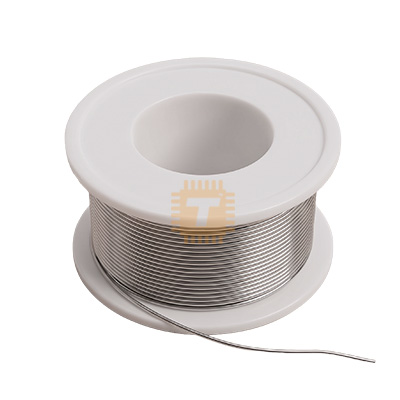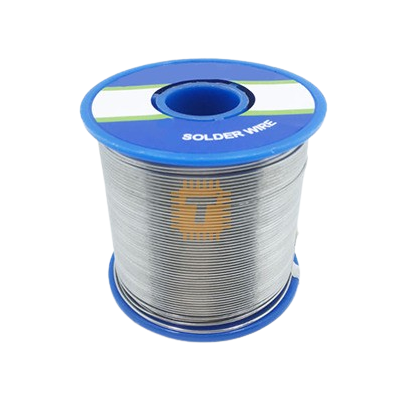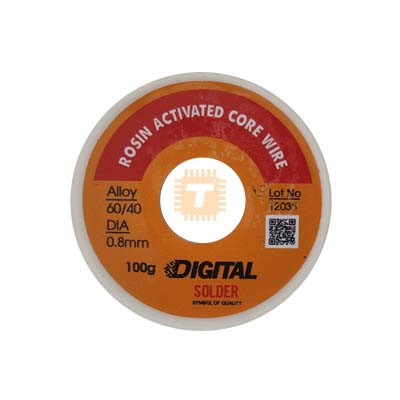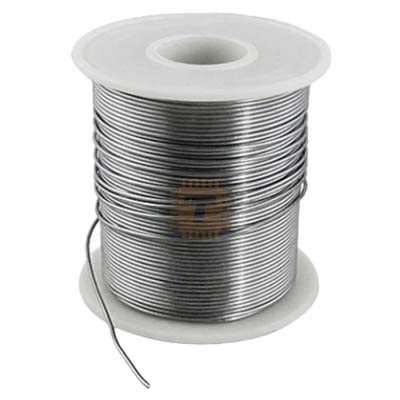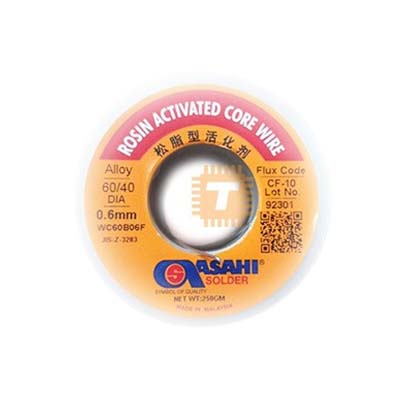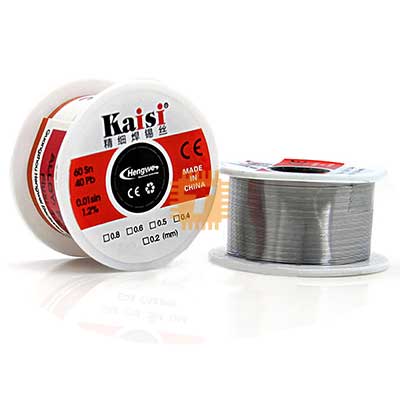
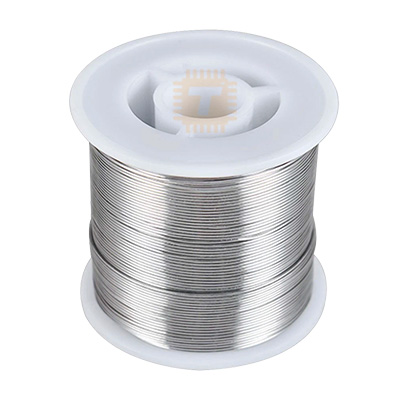
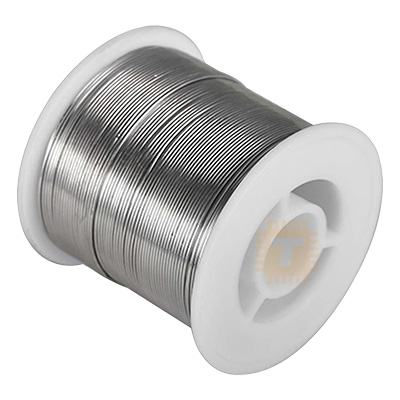
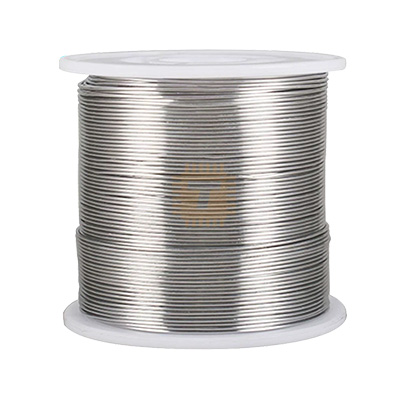
Solder Wire Lead Roll 63/37 0.8mm 1Kg
Price in Sri Lanka
Lead Solder Paste Flux and WicksTools and Accessories
Tronic.lk
Rs 14,750
In stock
Updated 01 Nov 2026
Opening hours
Open now
- Monday09:00 - 19:00
- Tuesday09:00 - 19:00
- Wednesday09:00 - 19:00
- Thursday09:00 - 19:00
- Friday09:00 - 19:00
- Saturday09:00 - 19:00
- SundayToday09:00 - 19:00
Search for it on
Description
The Solder Wire Lead Roll 63/37 0.8mm 1Kg is an industrial bulk spool of true eutectic tin-lead alloy soldering wire engineered for continuous factory production lines, high-volume PCB assembly, professional electronic repair stations, and heavy-duty wire harness manufacturing. Formulated with an exact metallurgical ratio of 63% Tin (Sn) and 37% Lead (Pb), it features a sharp, singular eutectic melting transition at exactly 183°C (361°F), completely eliminating the semi-solid "pasty range" during solidification. Centered along its versatile 0.8mm wire gauge is a continuous, high-grade activated rosin flux core that delivers instantaneous surface deoxidation, rapid capillary draw, and mirror-bright, concave solder joints with zero disturbance defects.
Specifications
- Alloy Composition: 63% Tin (Sn) / 37% Lead (Pb) (True Eutectic Formulation)
- Wire Diameter Gauge: 0.8 mm (Approx. 0.031 Inches / Ideal balance for SMD and THT)
- Net Alloy Weight: 1.0 kg (1000 g / ~2.2 lbs excluding spool tare weight)
- Quality Standard: Industrial High Purity (Virgin alloy with uninterrupted flux core continuity)
- Melting Characteristics:
- Eutectic Melting Point: Exactly 183°C (361°F)
- Solidus Temperature: 183°C
- Liquidus Temperature: 183°C
- Pasty Range: 0°C (Transitions instantly from liquid to solid without intermediate plastic phase)
- Flux Core Type: High-Grade Activated Rosin Core (RA / RMA Type, Non-Corrosive)
- Flux Content / Percentage: 1.8% to 2.2% Core by Weight
- Flux Halide Content: < 0>
- Solder Joint Appearance: Mirror-Bright, Shiny, and Smooth Concave Fillet
- Residue Characteristics: Amber/Clear, Non-Conductive, and Non-Corrosive Rosin Residue
- Spool Construction: Heavy-Duty Industrial Thermoplastic Reel with Wide Flange & Central Arbor
- Spool Dimensions: Approx. 65 mm to 70 mm Flange Diameter × 60 mm to 65 mm Width (Arbor hole: ~19 mm to 20 mm)
- Gross Weight: Approx. 1.10 kg to 1.15 kg (Wire and heavy spool combined)
Features
- True Eutectic Solidification: Freezes instantly upon cooling past 183°C, completely eliminating disturbed or crystalline cold solder joints caused by accidental component vibration on the bench.
- Bulk 1kg Industrial Capacity: Sized specifically for high-throughput assembly benches, automated wire-feeding soldering stations, and busy repair shops, drastically reducing downtime spent swapping empty spools.
- Versatile 0.8mm Diameter: The industry-standard all-rounder gauge that supplies the ideal solder volume per millimeter for through-hole DIP ICs, passive components, terminal blocks, pin headers, and medium SMD footprints (1206/0805).
- Instant Wetting & Capillary Flow: High-purity tin-lead alloy combined with an active rosin core strips surface oxidation from copper pads, brass terminals, and tinned leads in under a second.
- Non-Corrosive High-Impedance Residue: Dries into an inert, non-conductive rosin shield with high surface insulation resistance (SIR), safe to leave on standard commercial boards without fear of trace degradation.
- Low Spatter & Minimal Fuming: Carefully formulated flux core minimizes popping, solder spatter, and micro-balling during rapid thermal contact, keeping surrounding circuit boards clean.
Common Applications
- Industrial PCB Manufacturing: Hand-soldering and secondary touch-up for wave-soldered through-hole assemblies, power boards, and connector arrays.
- High-Volume Electronics Repair & Service: Continuous benchtop maintenance in consumer electronics repair centers, audio equipment restoration, and industrial automation service labs.
- Automated Wire Feeders: Compatible with motorized benchtop solder wire feeders paired with high-frequency induction soldering stations.
- Cable & Wire Harness Assembly: Tinning heavy-gauge stranded conductors, soldering automotive/marine harnesses, and assembling industrial multipin circular connectors.
- Robotics & Power Hardware: Soldering battery discharge leads (XT60, XT90), high-current ESC pads, motor terminals, and power distribution boards.
Usage Tips
- Iron Temperature Calibration:
- Due to the low eutectic melting point of 183°C, set your soldering iron tip between 300°C and 340°C (572°F to 644°F).
- Avoid operating above 360°C; excessive heat burns off the rosin core prematurely before it can clean the joint oxides, leaving frosty, dull solder surfaces.
- Proper Soldering Sequence:
- Touch the tinned iron tip simultaneously to the component lead and the PCB copper pad to heat both parts for 1 to 2 seconds.
- Feed the 0.8mm solder wire directly into the heated joint—not directly onto the iron tip. Once the solder flows smoothly around the lead to form a shiny concave fillet, withdraw the wire first, then cleanly lift the iron tip away.
- Spool Stand & De-Reeling Setup:
- Due to the substantial 1kg mass, mount the spool horizontally on a sturdy, bearing-supported benchtop solder reel stand.
- Pulling directly from an unsupported 1kg roll can bend the wire or cause the heavy spool to tip over and damage benchtop equipment.
- Residue Cleaning (Optional): While the rosin flux residue is non-conductive and chemically non-corrosive under normal operating conditions, clean sensitive RF, high-impedance analog, or high-voltage circuits using an ESD-safe brush and Isopropyl Alcohol (IPA ≥ 99%).
- Health & Environmental Safety:
- Contains elemental lead (Pb). Always wash hands thoroughly with soap and water after handling solder wire, and never eat or drink near the soldering workbench.
- Work in a well-ventilated space or use an active benchtop solder fume extractor to pull rosin flux smoke and airborne particulate away from your breathing zone.
Frequently asked questions
What is the price of Solder Wire Lead Roll 63/37 0.8mm 1Kg in Sri Lanka?▾
The current price of Solder Wire Lead Roll 63/37 0.8mm 1Kg in Sri Lanka is Rs 14,750 at Tronic.lk.
Is Solder Wire Lead Roll 63/37 0.8mm 1Kg available in Sri Lanka?▾
Yes, Solder Wire Lead Roll 63/37 0.8mm 1Kg is currently in stock at Tronic.lk in Sri Lanka.
Where can I buy Solder Wire Lead Roll 63/37 0.8mm 1Kg in Sri Lanka?▾
You can buy Solder Wire Lead Roll 63/37 0.8mm 1Kg in Sri Lanka at Tronic.lk. Visit 37left.lk to compare prices across multiple shops and find the best deal.
Loading...