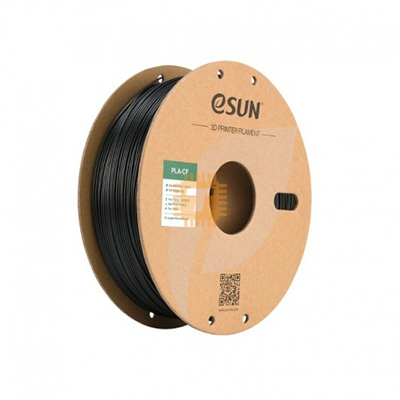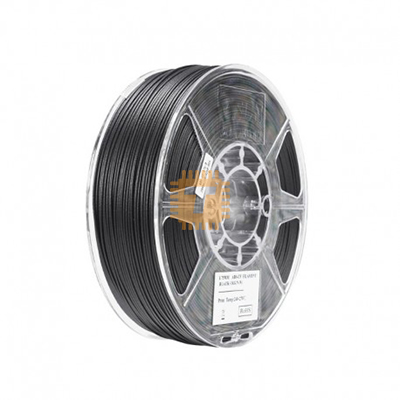
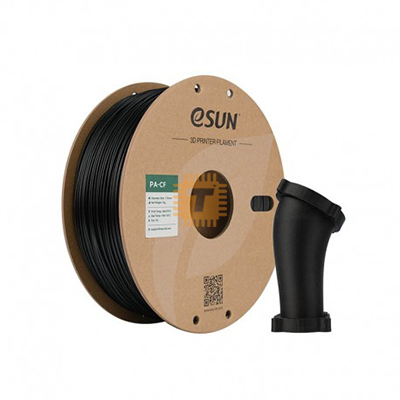
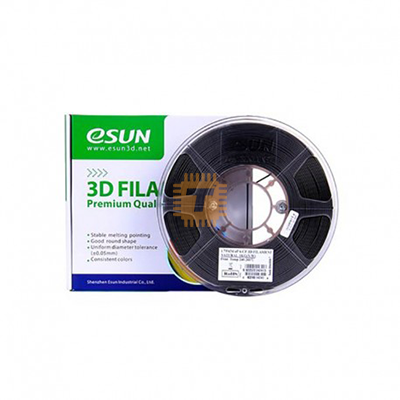
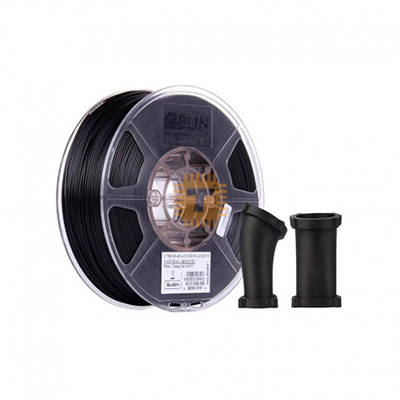
eSUN ePA-CF Carbon Fiber Black 1.75mm 1Kg 3D Printer Filament (Nylon Based)
Price in Sri Lanka
3D Printer FilamentsCNC and 3D Printers
Tronic.lk
Rs 14,500
In stock
Updated 01 Nov 2026
Opening hours
Closed now
- Monday09:00 - 19:00
- Tuesday09:00 - 19:00
- Wednesday09:00 - 19:00
- Thursday09:00 - 19:00
- Friday09:00 - 19:00
- Saturday09:00 - 19:00
- SundayToday09:00 - 19:00
Search for it on
Description
The eSUN ePA-CF Carbon Fiber Black 1.75mm 1kg 3D Printer Filament is an industrial-grade, carbon-fiber-reinforced engineering polymer designed for high-stress functional prototyping and end-use manufacturing on desktop and industrial FDM 3D printers. Formulated with a tough Polyamide (Nylon 6/66) base matrix compounded with 20% high-modulus chopped carbon fiber strands, this filament delivers exceptional tensile strength, extreme rigidity, superior heat resistance, and a premium matte black textured surface finish.
Specification
- Brand / Manufacturer: eSUN
- Product Name: ePA-CF Carbon Fiber Reinforced Nylon Filament
- Color Profile: Matte Carbon Black
- Filament Diameter: 1.75mm (Dimensional accuracy within ±0.03mm)
- Net Weight: 1.0 kg (2.2 lbs) spool
- Base Polymer Matrix: Polyamide (PA / Nylon) reinforced with approx. 20% chopped carbon fiber
- Recommended Extruder / Nozzle Temperature: 260°C to 300°C
- Recommended Heated Bed Temperature: 80°C to 100°C
- Recommended Chamber Temperature: Enclosed printing recommended (40°C to 60°C)
- Printing Speed Range: 30mm/s to 60mm/s (Up to 100mm/s+ on high-speed tuned machines)
- Cooling Fan Speed: 0% to 20% (Fan OFF recommended for maximum layer bonding)
- Heat Deflection Temperature (HDT): Approx. 155°C - 160°C (at 0.45 MPa)
- Tensile Strength: Approx. 110 - 140 MPa
- Flexural Modulus: Approx. 5500 - 6500 MPa
- Impact Strength (Izod): Approx. 8.5 kJ/m²
- Spool Material: High-Temperature Resistant Spool (Oven / Dryer Bake-Safe)
Features
- Extreme Structural Rigidity and Toughness: The 20?rbon fiber infill dramatically enhances the flexural modulus and tensile strength of the nylon base, producing parts capable of replacing CNC-machined aluminum in lightweight structural assemblies.
- High Thermal Deflection Resistance: Boasts an impressive heat resistance profile with heat deflection temperatures exceeding 150°C, ensuring mechanical stability in high-temperature engine bays, machinery housings, and baking environments.
- Significantly Reduced Warping Compared to Neat Nylon: Chopped carbon fibers restrict the thermal expansion and shrinkage tendencies of nylon during cooling, greatly improving dimensional stability and bed adhesion.
- Stunning Matte Texture and Layer Line Masking: Delivers a clean, non-reflective micro-textured surface that effectively conceals layer boundaries, producing parts with a factory injection-molded appearance.
- Superior Chemical and Wear Resistance: Retains the natural wear-resistant and self-lubricating characteristics of polyamide, showing robust resistance to oils, greases, fuels, and industrial solvents.
Common Applications
- Automotive & Motorsport Components: Fabricating lightweight under-hood brackets, intake manifolds, sensor housings, and custom ducting exposed to continuous heat and vibrations.
- Aerospace, Drones & Robotics: Manufacturing high-stiffness drone arms, motor mounts, robotic grippers, gear housings, and end-of-arm tooling (EOAT).
- Industrial Jigs, Fixtures & Tooling: Producing rigid manufacturing guides, press-brake inserts, assembly fixtures, and heavy-duty replacement machinery components.
Professional Installation and Maintenance Tips
- Mandatory Abrasion-Resistant Nozzle: Carbon fiber strands will erode standard brass nozzles within hours of printing. Always use a hardened steel, tungsten carbide, or ruby-tipped nozzle (minimum 0.4mm, with 0.6mm strongly recommended to prevent clogging).
- Bake and Dry Thoroughly Before Printing: Polyamide is intensely hygroscopic. Always bake the filament in an active filament dryer or oven at 70°C to 80°C for 6 to 10 hours prior to printing. For best results, print directly from a sealed, heated dry box.
- Use Bed Adhesion Enhancers on High-Temp Surfaces: Apply a high-temp bed adhesive (such as Magigoo PA, specialized bed glue, or PVP-based adhesive spray) onto a PEI, smooth glass, or FR4/Garolite build plate heated to 85°C - 95°C to ensure zero edge lifting.
- Enclose the Build Volume: While ePA-CF warps far less than standard nylon, an enclosed build chamber (around 40°C to 50°C) with part cooling fans turned OFF ensures maximum interlayer bonding and prevents delamination under heavy structural loads.
Frequently asked questions
What is the price of eSUN ePA-CF Carbon Fiber Black 1.75mm 1Kg 3D Printer Filament (Nylon Based) in Sri Lanka?▾
The current price of eSUN ePA-CF Carbon Fiber Black 1.75mm 1Kg 3D Printer Filament (Nylon Based) in Sri Lanka is Rs 14,500 at Tronic.lk.
Is eSUN ePA-CF Carbon Fiber Black 1.75mm 1Kg 3D Printer Filament (Nylon Based) available in Sri Lanka?▾
Yes, eSUN ePA-CF Carbon Fiber Black 1.75mm 1Kg 3D Printer Filament (Nylon Based) is currently in stock at Tronic.lk in Sri Lanka.
Where can I buy eSUN ePA-CF Carbon Fiber Black 1.75mm 1Kg 3D Printer Filament (Nylon Based) in Sri Lanka?▾
You can buy eSUN ePA-CF Carbon Fiber Black 1.75mm 1Kg 3D Printer Filament (Nylon Based) in Sri Lanka at Tronic.lk. Visit 37left.lk to compare prices across multiple shops and find the best deal.
Loading...