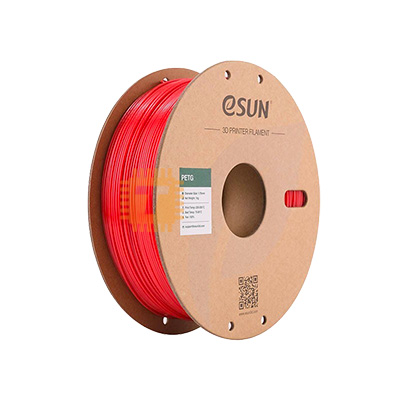
eSUN PETG Red 1.75mm 1Kg 3D Printer Filament Price in Sri Lanka
Tronic.lkListing · checkedChecked 10 Nov 2026
Rs4,500Out of stock
Go to Tronic.lk ↗https://tronic.lk/product/esun-petg-red-1-75mm-1kg-3d-printer-filamentCall0777854444WhatsApp+94764485607
Search for it on
Price history
Price at Tronic.lk at the end of each day · last 90 daysNo price history yetWe started tracking this listing recently. The chart and change tables appear after the first price or stock change.
Price insights
- Today at Tronic.lk
- Rs4,500
Description
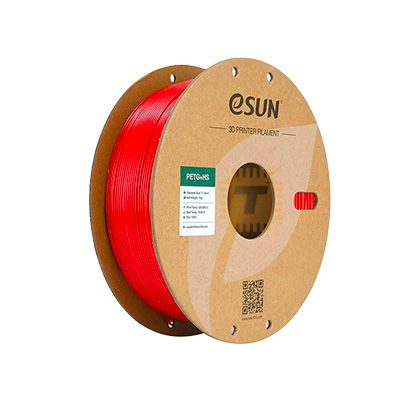
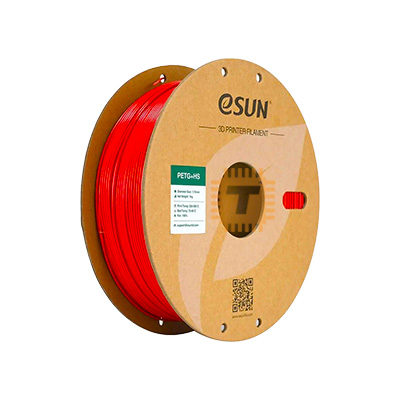
The eSUN PETG Red 1.75mm 1Kg 3D Printer Filament is an engineering-grade thermoplastic polyester filament engineered for durable functional prototypes, mechanical brackets, outdoor fixtures, and high-impact end-use components. Synthesized by copolymerizing standard polyethylene terephthalate (PET) with glycol (PETG), it eliminates the inherent brittleness of unmodified PET while combining the dimensional stability and ease of printing associated with PLA with the mechanical toughness, heat resistance, and chemical resilience of ABS. Housed on an environmentally friendly cardboard spool, this 1.75mm filament delivers consistent extrusion diameter (±0.03mm), high interlayer bonding strength, low shrinkage, and a vibrant, semi-translucent glossy red finish.
Specifications
- Material Formulation: Polyethylene Terephthalate Glycol-Modified (PETG)
- Filament Color: Red
- Filament Diameter: 1.75 mm (±0.03 mm high-precision laser-monitored tolerance)
- Net Material Weight: 1.0 kg (1000 g / ~2.2 lbs excluding spool tare mass)
- Density: Approx. 1.27 g/cm³
- Thermal Characteristics:
- Extrusion / Nozzle Printing Temperature: 230°C to 250°C (Recommended baseline: 240°C)
- Heated Bed Temperature: 70°C to 85°C (Recommended baseline: 75°C to 80°C)
- Heat Deflection Temperature (HDT): Approx. 68°C to 72°C (at 0.45 MPa)
- Glass Transition Temperature (Tg): ~80°C
- Mechanical Performance:
- Tensile Strength: ≥ 45 to 50 MPa
- Elongation at Break: ≥ 120% to 150% (High ductibility and fracture resistance)
- Flexural Modulus: ~2100 MPa
- Izod Notched Impact Strength: Approx. 7 to 8 kJ/m²
- Printing Speed Compatibility: 40 mm/s to 100 mm/s (Standard kinematics) / Up to 150–250 mm/s on high-flow CoreXY systems with tuned pressure advance
- Cooling Fan Speed: 30% to 60% (Lower fan speeds maximize layer adhesion; higher fan speeds improve overhang details)
- Spool Construction: Eco-Friendly Recyclable Cardboard Spool with filament level sight-gauges
- Spool Dimensions: Approx. 200 mm Outer Diameter × 65 mm Width (Arbor hub bore: ~53 mm)
- Packaging: Vacuum-sealed bag with desiccant pouch inside a retail corrugated box
- Gross Package Weight: Approx. 1.25 kg to 1.30 kg
Features
- Superior Layer-to-Layer Fusion: Fuses chemically and thermally across layer boundaries with virtually zero inter-layer separation, producing monolithic, watertight parts that withstand mechanical shear and hydrostatic pressure.
- High Ductility & Impact Resistance: Exhibits high tensile elongation (>120%) that yields elastically under sudden impact or cyclic loading rather than shattering abruptly like standard PLA.
- Moisture & Chemical Endurance: Chemically inert and resistant to diluted acids, alkalis, alcohols, automotive greases, and continuous water immersion, making it suitable for wet and humid environments.
- UV & Weather Resilience: Naturally resists ultraviolet light degradation, retaining structural rigidity and color saturation when deployed in direct outdoor sunlight.
- Low Warping & Shrinkage: Displays a minimal coefficient of thermal expansion, printing large, flat footprint parts on open-frame or enclosed beds without the severe edge lifting typical of ABS/ASA.
- Tangle-Free Precision Winding: Neatly layer-wound on high-speed automated spooling machines to eliminate crossed loops and snag-induced mid-print extruder clogs.
Common Applications
- Functional Mechanical Assemblies: Motor mounting brackets, drone frame arms, robotics chassis plates, belt tensioners, and structural pipe clamps.
- Outdoor & Marine Enclosures: Weatherproof sensor housings, agricultural monitoring enclosures, garden irrigation joints, and solar panel junction boxes.
- Automotive Interior & Engine Bay Accessories: Cup holder adapters, cable organizers, duct manifolds, and dashboard sensor clips that resist warm cabin temperatures up to ~70°C.
- Liquid Reservoirs & Fluidics: Custom water-cooling reservoirs, aquarium filter adapters, chemical funnel tubes, and hydroponic drainage nozzles.
- Electronics Prototyping: Custom snap-fit housings for development boards (Arduino, ESP32, Raspberry Pi) and heavy-duty hand-held device shells.
Usage Tips
- Build Plate Adhesion & Surface Protection (CRITICAL):
- NEVER print PETG directly onto a smooth, bare PEI sheet or clean glass bed without a release interface. PETG forms a molecular bond with smooth PEI and glass that can tear off the coating or take divots out of the glass upon part removal.
- Always apply a thin, uniform barrier layer using a PVP glue stick, Magigoo, or hairspray, or switch to a Textured Powder-Coated PEI flex sheet.
- Wait for the heated bed to cool down completely below 35°C before attempting to remove the printed object; it will often release on its own once cool.
- Mitigating Stringing & Oozing:
- PETG is inherently more viscous and prone to stringing than PLA.
- For direct-drive extruders, set retraction distance to 0.8 mm to 1.5 mm at 35–45 mm/s; for Bowden extruders, use 4.0 mm to 6.0 mm at 40–50 mm/s.
- Enable "Wipe While Retracting" and "Avoid Crossing Perimeters / Combing" in your slicer (OrcaSlicer, PrusaSlicer, or Cura) to wipe the nozzle tip over infill rather than outer walls.
- Z-Offset & Extruder Squish Calibration:
- PETG prefers to be laid down smoothly rather than heavily compressed (squished) into the bed like PLA.
- Raise your Z-offset by approximately +0.02 mm to +0.05 mm relative to a standard PLA calibration to prevent molten PETG from curling up around the nozzle heater block and creating burnt blobs.
- Filament Drying & Moisture Control:
- PETG is hygroscopic and absorbs ambient humidity from the air, resulting in popping sounds at the nozzle, heavy stringing, and a dull, foamy surface finish.
- If the spool has been exposed to open air, dry it in a dedicated filament dryer or convection oven at 60°C to 65°C for 6 to 8 hours prior to printing, and store the roll in an airtight container with active silica gel desiccant.
- Part Cooling Fan Optimization: Keep the cooling fan running between 20% and 50% for standard structural prints to preserve inter-layer bond strength. Only scale the fan up to 70%–100% on bridge spans and steep overhangs (>55°).
Questions
About this listing at Tronic.lkWhat is the price of eSUN PETG Red 1.75mm 1Kg 3D Printer Filament at Tronic.lk in Sri Lanka?
Rs 4,500, checked 10 Nov 2026.
Is eSUN PETG Red 1.75mm 1Kg 3D Printer Filament in stock at Tronic.lk in Sri Lanka?
No, it was out of stock at Tronic.lk at the last check.
Where can I buy eSUN PETG Red 1.75mm 1Kg 3D Printer Filament in Sri Lanka?
Tronic.lk sells it on tronic.lk. You can also call or WhatsApp the shop during opening hours.
Rs4,500at Tronic.lk · Out of stock
Go to Tronic.lk ↗https://tronic.lk/product/esun-petg-red-1-75mm-1kg-3d-printer-filament