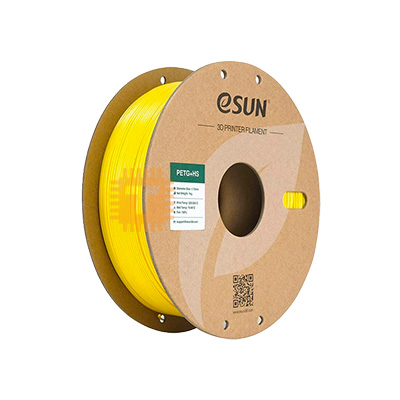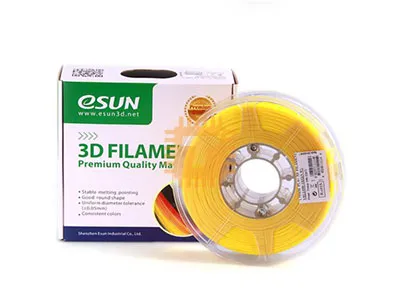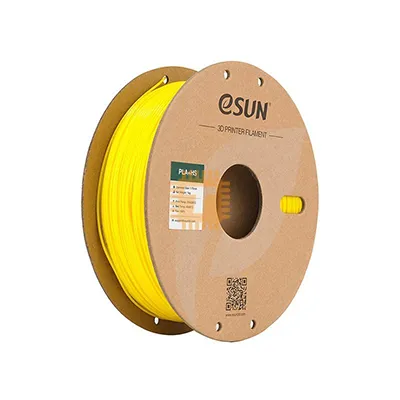
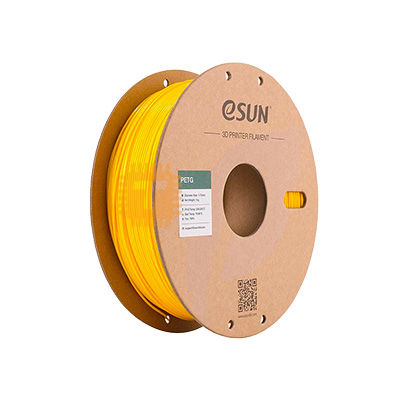
eSUN PETG Yellow 1.75mm 1Kg 3D Printer Filament Price in Sri Lanka
Tronic.lkListing · checkedChecked 10 Nov 2026
Rs4,500In stock
Go to Tronic.lk ↗https://tronic.lk/product/esun-petg-yellow-1-75mm-1kg-3d-printer-filamentCall0777854444WhatsApp+94764485607
Search for it on
Price history
Price at Tronic.lk at the end of each day · last 90 daysNo price history yetWe started tracking this listing recently. The chart and change tables appear after the first price or stock change.
Price insights
- Today at Tronic.lk
- Rs4,500
Description
The eSUN PETG Yellow 1.75mm 1Kg 3D Printer Filament is an engineering-grade thermoplastic polyester filament engineered for durable functional prototypes, safety fixtures, robotic chassis components, and high-visibility outdoor assemblies. Formulated by copolymerizing standard polyethylene terephthalate with glycol (PETG), it prevents crystallization and embrittlement while uniting the dimensional stability and ease of printing associated with PLA with the impact toughness, thermal endurance, and chemical resilience of ABS. Spooled onto an eco-friendly recyclable cardboard spool, this 1.75mm filament provides a tight diameter tolerance (±0.03mm), high interlayer bonding strength, low thermal shrinkage, and a vibrant, semi-translucent glossy canary yellow finish.
Specifications
- Material Formulation: Polyethylene Terephthalate Glycol-Modified (PETG)
- Filament Color: Yellow
- Filament Diameter: 1.75 mm (±0.03 mm high-precision laser-monitored tolerance)
- Net Material Weight: 1.0 kg (1000 g / ~2.2 lbs excluding spool tare mass)
- Density: Approx. 1.27 g/cm³
- Thermal Characteristics:
- Extrusion / Nozzle Printing Temperature: 230°C to 250°C (Recommended baseline: 240°C)
- Heated Bed Temperature: 70°C to 85°C (Recommended baseline: 75°C to 80°C)
- Heat Deflection Temperature (HDT): Approx. 68°C to 72°C (at 0.45 MPa)
- Glass Transition Temperature (Tg): ~80°C
- Mechanical Performance:
- Tensile Strength: ≥ 45 to 50 MPa
- Elongation at Break: ≥ 120% to 150% (High ductility, resists brittle fracturing)
- Flexural Modulus: ~2100 MPa
- Izod Notched Impact Strength: Approx. 7 to 8 kJ/m²
- Printing Speed Compatibility: 40 mm/s to 100 mm/s (Standard kinematics) / Up to 150–250 mm/s on high-flow CoreXY systems with tuned pressure advance
- Cooling Fan Speed: 30% to 60% (Lower speeds promote maximum inter-layer fusion; higher speeds improve bridge spans and overhangs)
- Spool Construction: Recyclable Eco-Friendly Cardboard Spool with filament weight sight-gauges
- Spool Dimensions: Approx. 200 mm Outer Diameter × 65 mm Width (Arbor hub bore: ~53 mm)
- Packaging: Vacuum-sealed bag with desiccant pouch inside a retail corrugated box
- Gross Package Weight: Approx. 1.25 kg to 1.30 kg
Features
- Superior Layer-to-Layer Adhesion: Melts and bonds aggressively across adjacent layer tracks, forming dense, watertight parts that resist shear failure and delamination under load.
- High Ductility & Impact Resistance: Resists fracturing under high-strain dynamic impacts by flexing elastically rather than snapping like standard rigid PLA.
- Chemical & Environmental Resilience: Inert to dilute acids, alkalis, greases, oils, and continuous water exposure, making it well-suited for industrial machinery and agricultural systems.
- UV & Weathering Endurance: Resists yellowing shift and mechanical embrittlement from solar ultraviolet radiation, maintaining bright yellow coloration in outdoor field installations.
- Low Warping & Shrinkage: Displays a minimal thermal expansion coefficient, enabling consistent flat prints on both enclosed and open-frame printers without extreme edge warping.
- Precision Layer Winding: Spooled with computer-controlled tension winding to prevent overlapping loops, tangles, and mid-print feed jams.
Common Applications
- Safety Fixtures & Warning Housings: High-visibility end-stop indicators, emergency stop button guards, lock-out/tag-out (LOTO) clips, and caution guides in workshop environments.
- Robotics & Drone Platforms: Structural drone arms, motor mounts, battery cradles, and robot bumpers requiring both high impact tolerance and bright orientation visibility.
- Outdoor & Agricultural Enclosures: Weatherproof sensor enclosures, telemetry beacons, and automated irrigation brackets exposed to sunlight and moisture.
- Automotive & Workshop Accessories: Custom tool holders, fluid reservoir brackets, and duct adapters that resist engine bay/cabin heat up to ~70°C.
- Custom Electronics Enclosures: Vibrant, protective shells for DIY hardware projects, Arduino/ESP32 sensor modules, and field-testing cases.
Usage Tips
- Build Plate Adhesion & Surface Protection (CRITICAL):
- Do NOT print PETG directly onto smooth PEI or clean bare glass without a separation barrier. PETG bonds aggressively to smooth PEI and glass surfaces and can rip chunks out of the coating or glass plate during removal.
- Apply a thin release layer of PVP glue stick, Magigoo, or hairspray, or switch to a Textured Powder-Coated PEI spring steel sheet.
- Wait until the heated bed cools completely below 35°C before taking the part off; it will typically release on its own once cool.
- Retraction & Stringing Prevention:
- Due to PETG's high melt viscosity, dial in retraction to prevent fine cobwebs and oozing.
- For direct-drive setups, use 0.8 mm to 1.5 mm retraction at 35–45 mm/s; for Bowden extruders, use 4.0 mm to 6.0 mm at 40–50 mm/s.
- Enable slicer features like "Wipe While Retracting" and "Avoid Crossing Perimeters" (Combing) to wipe the nozzle tip over internal infill before traveling over outer shells.
- Z-Offset Calibration:
- Unlike PLA, which benefits from being firmly squished into the build plate, PETG prefers to be laid down gently without excessive nozzle pressure.
- Increase your Z-offset by roughly +0.02 mm to +0.04 mm relative to a standard PLA calibration to keep molten plastic from sticking to the nozzle nozzle and causing burnt blobs.
- Drying & Humidity Management:
- PETG is hygroscopic and absorbs ambient moisture over time, resulting in popping sounds, foamy outer walls, and weak layer bonding.
- If the spool has been exposed to ambient humidity, dry it in an active filament dryer or convection oven at 60°C to 65°C for 6 to 8 hours before printing, and feed it from a sealed dry box for long multi-day jobs.
- Fan Speed Optimization: Run part cooling at 20% to 50% for general structural parts to maximize interlayer strength. Increase cooling to 60%–80% only during short layer times, bridging spans, and steep overhang angles (>55°).
Questions
About this listing at Tronic.lkWhat is the price of eSUN PETG Yellow 1.75mm 1Kg 3D Printer Filament at Tronic.lk in Sri Lanka?
Rs 4,500, checked 10 Nov 2026.
Is eSUN PETG Yellow 1.75mm 1Kg 3D Printer Filament in stock at Tronic.lk in Sri Lanka?
Yes, it was in stock at Tronic.lk at the last check.
Where can I buy eSUN PETG Yellow 1.75mm 1Kg 3D Printer Filament in Sri Lanka?
Tronic.lk sells it on tronic.lk. You can also call or WhatsApp the shop during opening hours.
Rs4,500at Tronic.lk · In stock
Go to Tronic.lk ↗https://tronic.lk/product/esun-petg-yellow-1-75mm-1kg-3d-printer-filament